

Feedback
Autrice: FTM
Data: Sep 16, 2026
Come funziona la fusione in sabbia? Fasi del processo, materiali e applicazioni chiave
Sand casting is the most widely used metal casting process because it is simple, cost-effective, and capable of producing large, complex parts in nearly any ferrous or non-ferrous alloy. The core principle is straightforward: a cavity in a sand mold replicates the desired shape, molten metal fills that cavity, and after solidification the sand is broken away to reveal the finished casting. This process works for parts ranging from a few kilograms to several tons, making it indispensable for industries such as agricultural machinery, automotive, construction equipment, and marine hardware.
Il principio base della fusione in sabbia
At its simplest, sand casting works by creating a reusable pattern that is pressed into a mixture of sand and binder to form a mold. The pattern is removed, leaving a cavity exactly matching the part geometry. A gating system—consisting of sprues, runners, and gates—is also carved into the sand to guide molten metal into the cavity. Risers (reservoirs of molten metal) are added to compensate for shrinkage as the metal cools. After pouring and solidification, the mold is broken apart to extract the casting, which then undergoes cleaning, heat treatment, and any required machining.
Unlike permanent mold processes, sand casting uses a sacrificial mold that is destroyed after each pour. This is why it excels for low-to-medium volume production and for parts too large or intricate for die casting. The flexibility in mold size and metal selection directly benefits buyers who need  Custom Sand-Cast Flange Shafts for Heavy-Duty Use These flange shafts are produced via sand casting, offering flexibility in material selection like grey or ductile iron and size, ideal for custom heavy-duty applications without high tooling costs. Visualizza il prodotto → or other heavy-duty components without the high tooling costs of other methods.
Passo dopo passo: come funziona la fusione in sabbia
While the exact sequence can vary depending on the foundry and part complexity, the following eight steps represent the typical sand casting workflow.
1. Realizzazione di modelli
A pattern is a replica of the final part, usually made from wood, plastic, or metal. It is slightly oversized to account for shrinkage of the molten metal as it cools. Patterns can be single-piece or split into two halves (cope and drag). For internal cavities, cores made of sand are placed in the mold.
2. Preparazione dello stampo
The pattern is placed in a flask—a rigid frame—and sand mixed with a binder (commonly clay for green sand, or resin for no-bake sand) is compacted around it. The cope (top half) and drag (bottom half) are formed separately. After ramming, the pattern is withdrawn, leaving an exact negative cavity.
3. Progettazione del sistema di cancelli e montanti
Channels are cut into the sand to connect the cavity to the outside. The sprue receives the molten metal, which flows down a runner and through gates into the cavity. Risers are placed at thick sections to feed additional metal as the casting shrinks.
4. Posizionamento del nucleo (se necessario)
If the part has internal passages or undercuts, sand cores are inserted into the mold cavity before closing. I nuclei sono preformati e cotti per acquisire forza.
5. Assemblaggio dello stampo
The cope and drag are aligned and clamped together to prevent leakage. Lo stampo è ora pronto per la colatura.
6. Versamento del metallo fuso
The metal (iron, steel, aluminum, bronze, etc.) is melted in a furnace and poured into the sprue at a controlled temperature and rate. The metal fills the cavity, risers, and gating system.
7. Raffreddamento e solidificazione
The casting is left to cool for a period determined by its wall thickness and metal type. Proper cooling time is critical to avoid defects such as porosity or cracks.
8. Shakeout e rifinitura
The sand mold is broken apart, typically by vibration or mechanical shaking. The casting is separated from the gating system and risers. Excess material is trimmed, and the surface is cleaned via shot blasting, grinding, or sanding. Ulteriori operazioni come trattamento termico, lavorazione e rivestimento potrebbero seguire per soddisfare le specifiche finali.
For a reliable supplier that handles the entire sand casting process—from pattern to finished machined part—consider sourcing from an experienced manufacturer like Ningbo Hansheng Machinery Parts Co., Ltd., which offers  Colata in sabbia di acciaio per hardware marino Sourced from an experienced manufacturer, these steel sand castings for marine hardware ensure stringent quality standards through collaboration with expert metallurgists and molders. Visualizza il prodotto → e molte altre applicazioni industriali.
Tipi di sabbia utilizzati nella fusione in sabbia
The choice of sand directly affects mold strength, surface finish, and cost. I tipi più comuni includono:
- Sabbia verde – a mixture of silica sand, clay, water, and additives. It is the cheapest and most widely used, suitable for ferrous and non-ferrous alloys.
- Sabbia di resina – sand bonded with a resin that cures chemically. It produces a smoother surface and tighter dimensional tolerances.
- Sabbia di silicato di sodio (bicchiere d'acqua). – bonded with sodium silicate and cured by CO₂ gas. Fornisce una buona resistenza e pieghevolezza.
- Sabbia secca – sabbia legata argillosa che viene cotta in forno. Più resistente della sabbia verde ma più costosa.
The table below summarizes key differences between the two most commonly used sand types in production.
| Proprietà | Sabbia verde | Sabbia di resina |
|---|---|---|
| Tipo di legante | Acqua di argilla | Resina sintetica |
| Resistenza allo stampo | Moderato | Alto |
| Finitura superficiale | Ruvido | Liscio |
| Precisione dimensionale | ±0,5–1,0 mm | ±0,3–0,5 mm |
| Costo per stampo | Basso | Moderato |
| Riciclabilità | Alto | Limitato |
Perché viene scelta la fusione in sabbia per le parti industriali
Engineers and procurement professionals turn to sand casting when they need large, heavy parts that cannot be economically produced by other methods. Il processo offre quattro vantaggi principali:
- Basso costo degli utensili – Patterns are relatively cheap compared to die-casting dies, making sand casting ideal for prototypes and short-to-medium production runs.
- Flessibilità dei materiali – Almost any metal can be cast: steel, iron, aluminum, bronze, magnesium, and even specialty alloys.
- Capacità di dimensione – Parts weighing hundreds of kilograms and measuring several meters are routine. Engine blocks, pump housings, and valve bodies are typical examples.
- Adattabilità del design – Modifications to the pattern are easy, allowing design changes without expensive retooling.
Tuttavia, la fusione in sabbia presenta dei limiti. Surface finish is rougher than die casting or investment casting, requiring secondary machining for critical surfaces. Tolerances are wider, typically ±0.5 mm or more. For applications where these factors are acceptable, sand casting delivers the best value. Un buon esempio è la produzione di 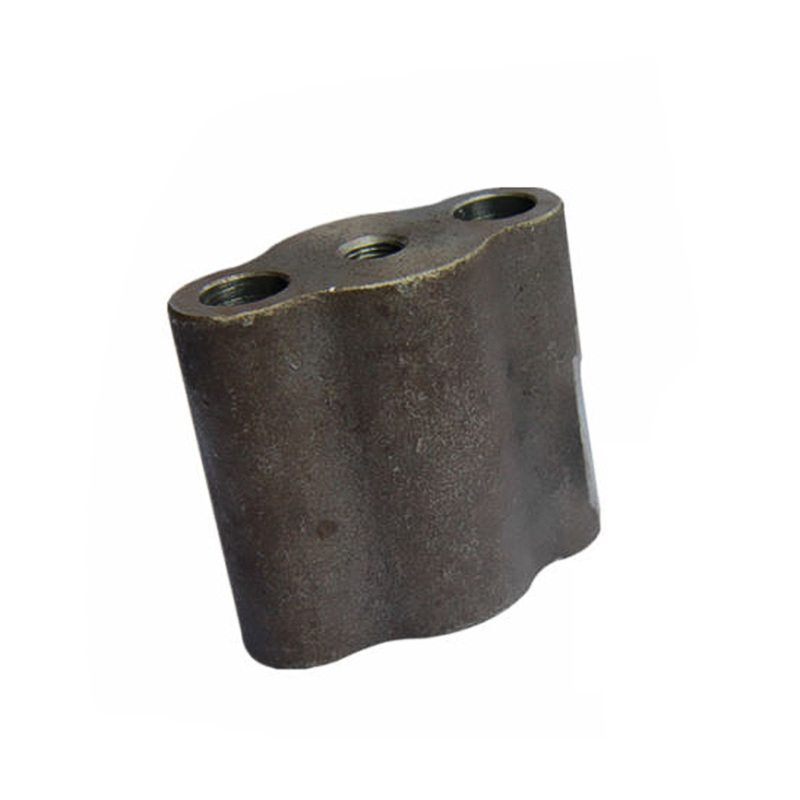 Parti del motore in fusione in sabbia per resistenza e costi For motor parts where strength and material cost matter more than surface finish, sand casting delivers reliable performance using a wide range of carbon and alloy steels. Visualizza il prodotto → , where strength and material cost take priority over surface aesthetics.
Applicazioni in settori chiave
Sand casting supports a vast range of industries. Based on the capabilities of manufacturers like Ningbo Hansheng, the following sectors frequently rely on sand-cast components:
- Macchine agricole – gear housings, plough shares, transmission casings.
- Automobilistico – engine blocks, cylinder heads, brake components.
- Edilizia e estrazione mineraria – bucket teeth, adapter plates, crusher wear parts.
- Marino e offshore – eliche, corpi valvola, corpi pompa.
- Macchinari industriali – machine tool bases, motor frames, hydraulic manifolds.
- Valvole e controllo dei fluidi – corpi valvola, flange, raccordi.
Each industry has its own requirements for material, tolerance, and post-processing. A reputable foundry will work with customers to select the appropriate sand type, alloy, and finishing operations, ensuring the final part meets both performance and budget targets.
Conclusion: The Practical Choice for Large Metal Parts
Sand casting works by leveraging a disposable sand mold to create metal parts with minimal upfront investment and maximum material versatility. The process is well understood, highly repeatable, and trusted by industries that demand strength and durability at scale. If you are evaluating manufacturing options for a heavy component, understanding how sand casting parts are applied in industrial manufacturing ti aiuterà a prendere una decisione informata.
For a partner that combines sand casting with CNC machining, heat treatment, and surface finishing under one roof, the expertise of a Chinese foundry with decades of export experience—such as Ningbo Hansheng Machinery Parts Co., Ltd.—can reduce your lead times and simplify supply chain management. Their product line includes numerous sand-cast components, from flange shafts to motor parts and marine hardware, all manufactured to international quality standards.
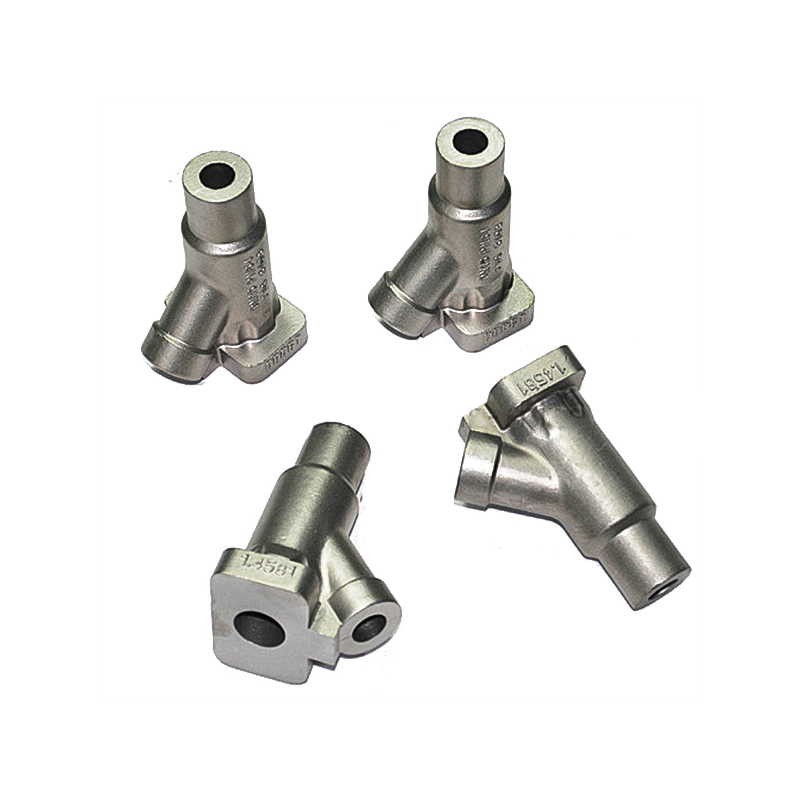
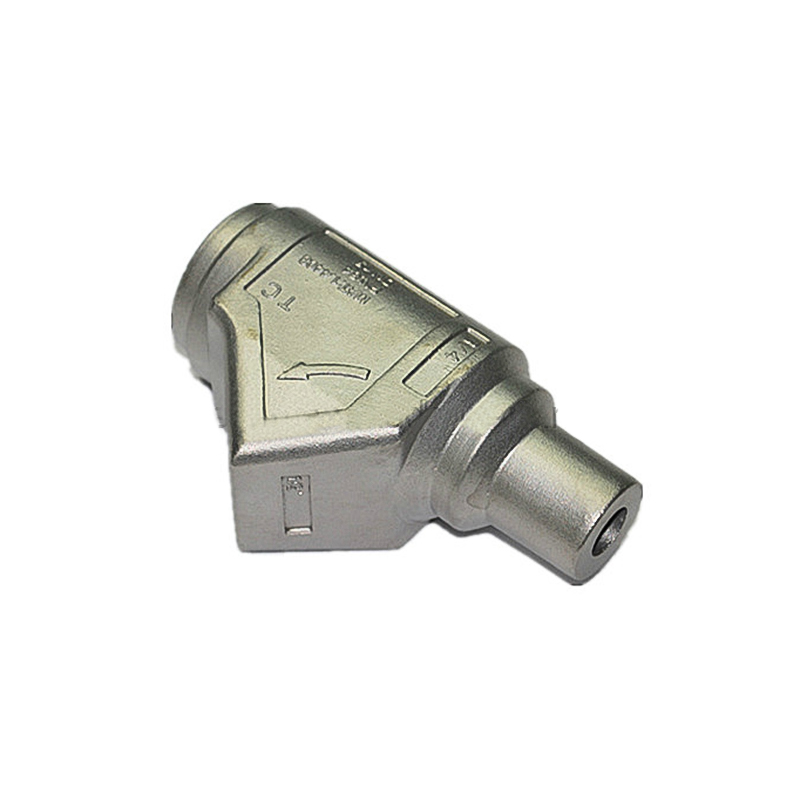
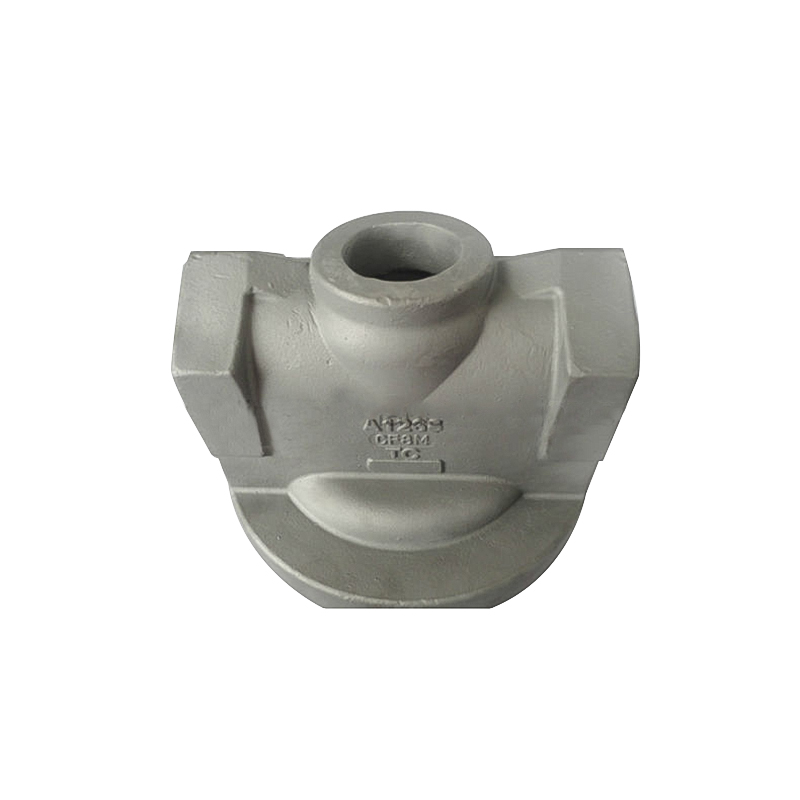
Visualizzazione del cuscinetto selezionato
Informazioni di contatto
- Tel:+86-574-88067800/88067900
- Fax:+86-574-88067400
- Phone:+86-13967874638
- E-Mail:master@nbyifei.com
Collegamenti ai prodotti
Collegamenti ai prodotti
- Parti di fusione di macchine agricole
- Parti di fusione automatica
- Parti in pressofusione di ottone
- Dente e accessorio della benna di fusione
- Parti di fusione del contenitore
- Parti di fusione di investimento
- Parti di fusione di macchinari
- Parti di fusione di macchine minerarie
- Parti di fusione di treni e ferrovie
- Parti di fusione in sabbia
- Parti per stampaggio e forgiatura
- Parti di fusione della valvola
Contattaci
Diritto d'autore©
Ningbo Hansheng Machinery Parts Co.,Ltd. Tutti i diritti riservati
 Produttori di pressofusioni personalizzate
